Core Value
In precision mold engineering, tooling plates are frequently stacked tightly, leaving negligible clearance between the heater insertion bore and adjacent machine components. When machine operators install standard straight cartridge heaters into these confined spaces, the exiting lead wires are immediately forced into an acute bend right at the edge of the sheath. This severe bending stress rapidly fractures the internal nickel conductor strands, crushes the high-temperature fiberglass insulation, and leads to direct electrical short circuits against the grounded mold base.
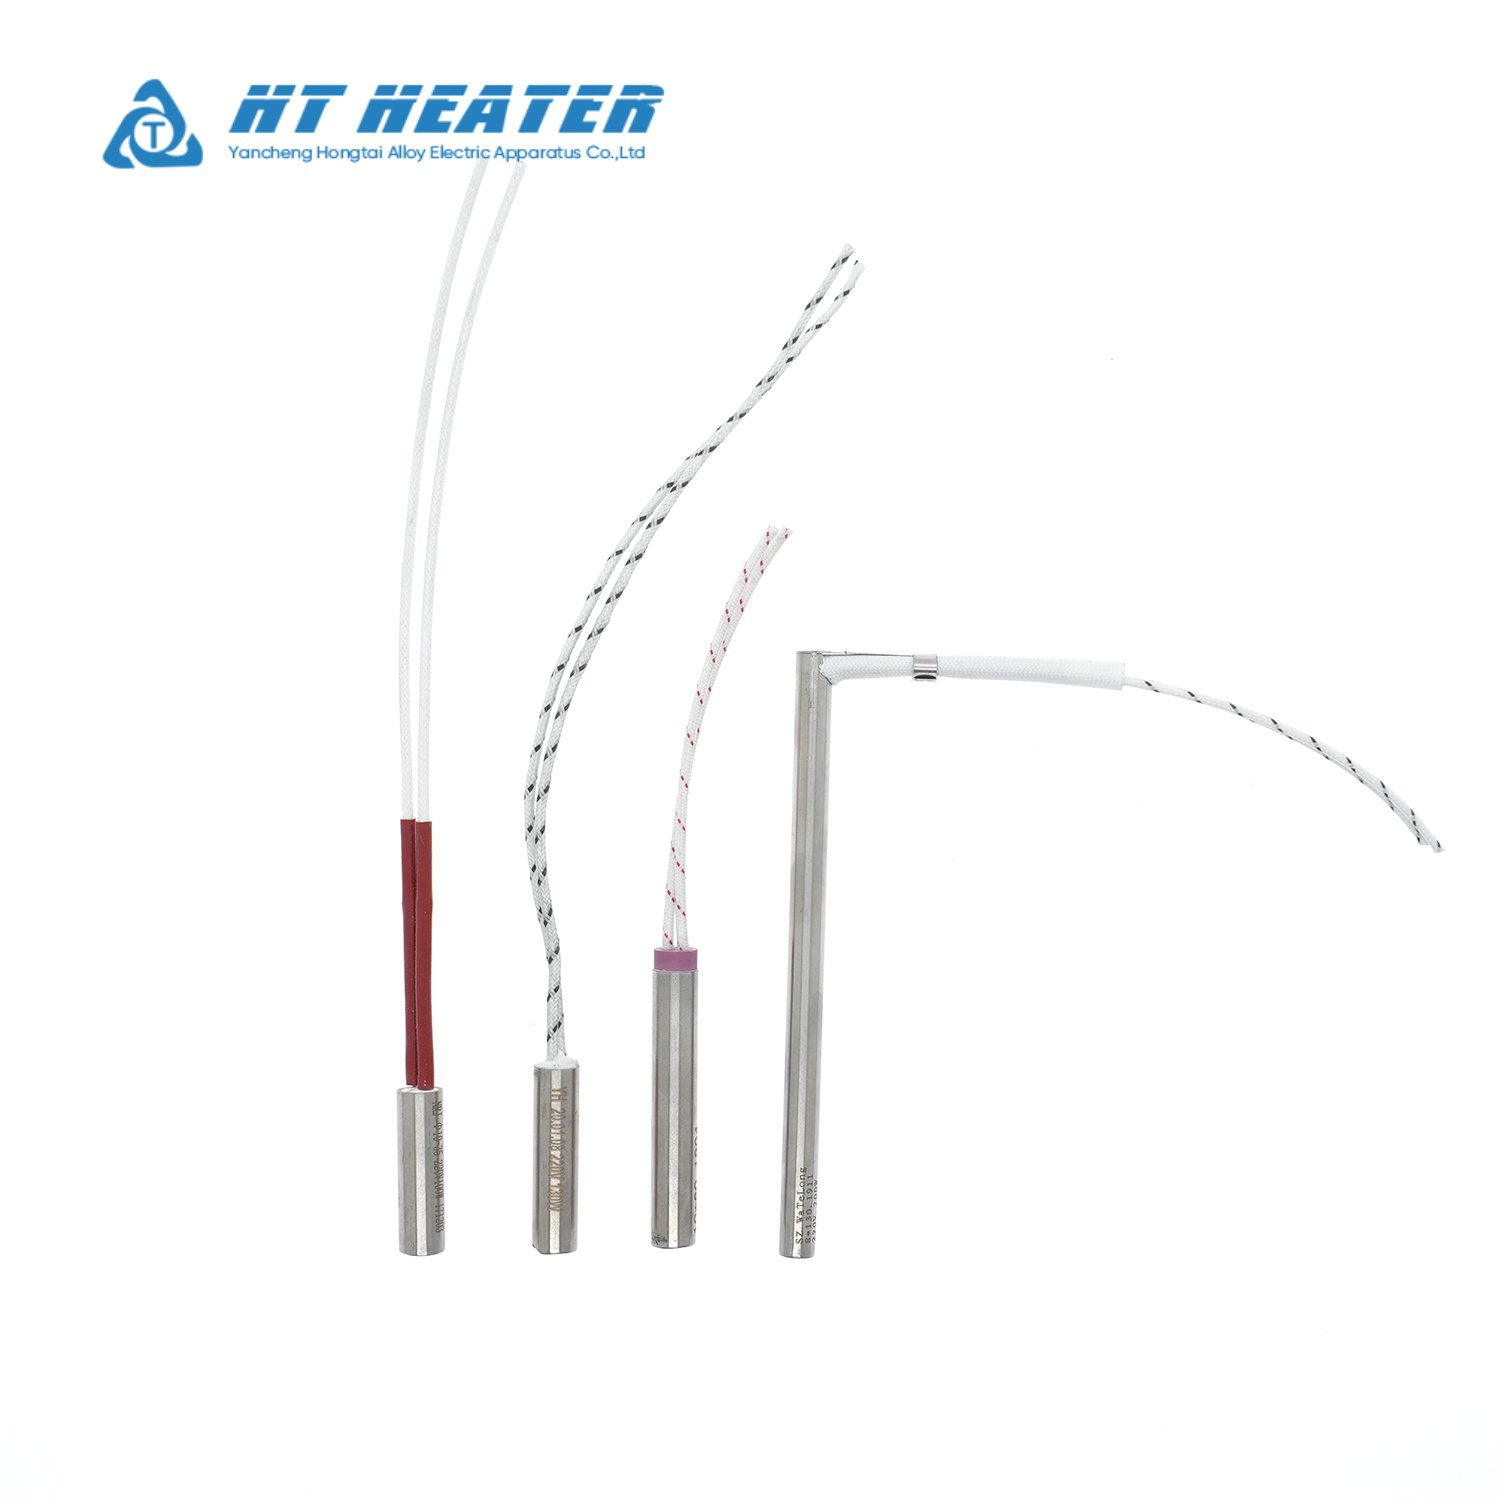
The Custom Shape Stainless Steel Cartridge Heater For Mold 220V definitively solves this clearance challenge. By engineering the lead exit at a permanent 90-degree angle via a reinforced stainless steel welded elbow or a machined transition block, the wiring runs parallel to the mold face immediately upon exiting the bore. This eliminates wire-bending fatigue, protects the lead insulation from mechanical pinch points, and allows molds to be designed with significantly slimmer plate profiles.
Internally, the heater incorporates high-compaction rotary swaging. A precision computer-wound Ni80Cr20 nickel-chromium resistance coil is centered on a high-purity refractory ceramic core, surrounded by electro-fused magnesium oxide (MgO) dielectric powder. Under multi-ton swaging forces, the assembly is compressed to near-theoretical crystalline density, establishing an ultra-conductive thermal path to the outer SUS304, SUS316L, or Incoloy sheath. This enables the unit to operate safely at high surface watt densities (15 to 30 W/cm2) and core temperatures up to 750°C.
To guarantee effortless sliding insertion and optimal conductive transfer, the stainless steel outer diameter undergoes high-precision centerless grinding, maintaining tight dimensional tolerances (within ±0.02mm). Depending on operating conditions, lead transitions can be configured with red high-temperature silicone sleeving for moisture protection, ceramic end caps for ultra-high radiant environments, or braided fiberglass sleeves for flexible handling.
- ✓ Space-Saving 90° Right-Angle Lead Exit: Eliminates wire-bending stress in tight mold plate clearances, preventing conductor fatigue and electrical short circuits.
- ✓ High-Compaction Rotary Swaged Core: Compresses electro-fused MgO to maximum density, maximizing conductive heat transfer and supporting watt densities up to 25–30 W/cm².
- ✓ Centerless Ground Sheath (±0.02mm): Machined to strict outer diameter tolerances for a close, low-clearance H7 slip-fit into reamed mold cavities.
- ✓ Engineered Transition Sealing: Available with ceramic end caps, high-temperature epoxy potting, or red silicone boot seals to guard against moisture, hydraulic oil, and plastic melt.
- ✓ TIG-Welded Hermetic End Disc: Deep 360-degree fusion welding on the bottom disc provides a pressure-tight seal that prevents fluid and polymer ingress.
- ✓ Direct OEM Manufacturing: Fully customizable sheath diameters, insertion lengths, lead protection options (fiberglass, silicone, armor cable), and dual-voltage designs produced by HT HEATER.
Technical Specifications & Performance Data
| Parameter | Standard Specification | Customizable Options | Engineering Notes |
| Product Category | Custom Shape / Right-Angle Cartridge Heater | Straight cartridge, flanged cartridge | Engineered for tight mold clearances |
| Operating Voltage | 220V AC Single Phase | 110V, 120V, 240V, 380V, 480V | 220V standard for global plastic injection tooling |
| Power Output (Wattage) | 100W to 1500W+ | Custom watt densities per tooling zone | Power balanced precisely across active heated length |
| Outer Diameter (Ø) | Φ6mm, Φ8mm, Φ10mm, Φ12mm to Φ25mm | Fractional imperial sizes (1/4″ to 1″) | Centerless ground to ±0.02mm for snug bore fit |
| Sheath Length ($L$) | 30mm to 1500mm+ Standard | CNC tailored to mold depth | Custom unheated cold zones available at tip or base |
| Lead Exit Configurations | 90° Right-Angle Elbow, Straight Exit | Offset block, bent sheath, dual-ended | Prevents wire bending against adjacent mold plates |
| Sheath Material | SUS304 Stainless Steel | SUS316L, Incoloy 800 / 840 | Incoloy recommended for operating temps 500°C |
| Internal Dielectric | High-Purity Swaged Crystalline MgO | – | Rotary compacted for maximum dielectric isolation |
| Lead Wire Types | High-Temp Fiberglass / Silicone Leads | Stainless steel braid, flexible conduit armor | Outfitted with protective silicone or ceramic sleeves |
| Internal Thermocouple | Optional Non-Sensor | Built-in Type J or Type K Thermocouple | Grounded to sheath or ungrounded at bottom disc |
Industrial Applications & Solutions
This space-saving custom right-angle cartridge heater is the specified thermal solution across precision tooling applications:
-
Multi-Cavity Plastic Injection Molds: Installed where tight plate stacking or hydraulic slide mechanisms leave minimal external clearance for wiring.
-
Hot Runner Manifolds & Drop Nozzles: Delivers direct, localized heating to melt channels without wiring interfering with nozzle retaining bolts.
-
Packaging & Blister Sealing Jaws: Fits into compact reciprocating sealing bars where moving mechanical linkages would snag straight exiting leads.
-
Die-Casting & Stamping Platens: Heats mold core pins, sprue bushings, and trimming dies to maintain uniform tool temperatures and prevent metal flow flaws.
-
Medical Diagnostic Platens: Provides compact, reliable thermal conduction inside space-restricted laboratory equipment and fluid analysis chambers.
HT Heater Advantage: Why Choose Our Cartridge Heater?
| Engineering Feature | HT Heater Custom Right-Angle Cartridge | Generic Cartridge Heaters | Operational Advantage |
| Elbow Transition Joint | TIG-welded structural stainless steel elbow | Bent standard sheath with cracked insulation | Prevents wire pinch and protects conductors from sharp internal metal edges during installation. |
| Dimensional Accuracy | Precision centerless ground to ±0.02mm | As-drawn tube with irregular roundness | Ensures a tight, uniform bore fit, maximizing heat dissipation and eliminating extraction seizing. |
| Internal Compaction | Multi-ton rotary swaging compaction | Loose, vibration-packed powder filling | Eliminates internal air gaps, lowering core wire operating temperatures and multiplying service lifespan. |
| Dielectric Testing | 100% factory flash tested (1000 MΩ @ 500VDC) | Random batch sampling | Guarantees zero leakage current and complete operator safety in grounded industrial machinery. |
Installation & Handling Guidelines
-
Precision Bore Clearance (H7 Fit): To ensure rapid conductive heat transfer and prevent overheating, the reamed hole diameter should not exceed the heater outer diameter by more than 0.08mm to 0.1mm (0.003″ to 0.004″). Air gaps act as thermal barriers that rapidly cause high-watt-density elements to burn out.
-
Handle Right-Angle Elbows Correctly: When inserting the cartridge heater into the mold bore, apply pushing force only along the central axis of the straight sheath. Never use the 90-degree elbow or exiting lead wires as a lever or hammer point, as this will damage the internal lead weld.
-
High-Temperature Thermal Paste: Apply a light, uniform coating of high-temperature heat transfer paste (anti-seize compound) to the cylindrical sheath before insertion. This fills microscopic surface voids, enhances heat dissipation, and prevents the heater from seizing in the tooling over time.
-
Lead Routing & Strain Relief: Secure the flexible lead wires along mold wireways using heat-resistant clamping brackets. Ensure leads are shielded from moving mold slides, sliding core pins, and corrosive polymer outgassing.
Customer Success Stories
Case 1:
Automotive Multi-Cavity Mold Maker (Germany)
-
Application: High-precision injection mold producing glass-filled nylon automotive wire harness connectors.
-
Challenge: Due to tightly spaced mold slides and ejector pin plates, the mold had less than 15mm of clearance outside the heater bores. Standard straight cartridge heaters suffered continuous lead wire crimping and internal short circuits during mold assembly, halting production lines every few weeks.
-
Solution: Partnered with HT HEATER to standardize the tooling on Custom 220V Right-Angle Stainless Steel Cartridge Heaters featuring welded 90-degree elbows and flexible fiberglass-sleeved leads.
-
Results: LEAD WIRE BREAKAGE COMPLETELY ELIMINATED. The low-profile 90-degree exit routed neatly through pre-machined mold wire channels with zero mechanical interference. Mold maintenance intervals extended past 18 months of continuous production.
Case 2:
High-Speed Blister Packaging OEM (United States)
-
Application: Reciprocating heat-sealing bars on pharmaceutical blister packaging machines operating at 100 cycles per minute.
-
Challenge: The compact sealing jaw assembly had moving mechanical arms that repeatedly caught and frayed straight-exit heater leads, causing ground faults and expensive downtime.
-
Solution: HT Heater supplied custom-length 220V cartridge heaters with reinforced right-angle transitions and abrasion-resistant red silicone protective sleeving.
-
Results: UNINTERRUPTED PACKAGING CYCLES. The right-angle profile kept all wiring flush against the stationary side of the sealing bar. With zero lead interference, the packaging lines achieved continuous three-shift operations with consistent ±1.0°C sealing jaw temperature uniformity.
Pricing & Procurement Options
- OEM Customization: Tailored shapes, custom cutout holes for pipe nozzles, specialized voltage/wattage configurations, and custom strap lengths.
- Lead Times: Custom samples: 3–5 working days. Bulk production orders: 8–12 working days upon technical drawing sign-off.
- Packaging & Shipping: Individually bagged with protective foam padding and packed into heavy-duty 5-ply export cartons to prevent bending or lead wire stress during international transit.
- Minimum Order Quantity (MOQ): Low MOQ starting at 5–10 units for custom dimensions; competitive volume pricing tiers for equipment manufacturers.
Global Certifications & Compliance
- CE Marking
Fully compliant with European safety and environmental standards. - LVD Compliance
Low Voltage Directive tested for continuous thermal load safety. - RoHS Compliant
Constructed using environmentally safe, lead-controlled brass alloys. - ISO 9001
Certified quality control covering CNC machining, coil pressing, and electrical testing.
Quality Documentation: Certificate of Conformity (COC) and insulation resistance test reports included.
Comprehensive After-Sales Support
-
- Warranty: 1-Year Comprehensive Warranty covering internal heating element and built-in sensor.
-
Technical Support: Application engineers available for wattage distribution calculation, thermocouple calibration, and nozzle fitting assistance.
-
Global Response Network: BACKED BY 30+ YEARS MANUFACTURING EXPERIENCE with technical inquiry feedback within 2 hours.
Ready to Optimize Your Injection Molding?
Next Steps:
- 📧 Request Custom Quote – Send your nozzle dimensions, wattage, voltage, and HT-CLW-450 drawing requirements.
- 🔧 Free Design Consultation – Work with our thermal engineers to optimize heat distribution and lead insulation.
- 📦 Order Test Samples – Evaluate thermal performance on your injection molding machine.
- 📞 Contact Hot Runner Experts – Response within 2 hours
-
Leading Manufacturer & Export of Industrial Heaters
Providing A One Stop Solutions To All Industrial Heaters Needs
SINCE 1990 Professional Heater Producer | Our Products Undergo Multiple Rigorous Quality Checks