Core Value
In modern plastics extrusion and injection molding of engineering-grade resins—such as PEEK, PPS, Polycarbonate (PC), Nylon (PA6/PA66), and fluoropolymers—barrel zone temperatures routinely exceed 350°C to 450°C. Standard mica band heaters rely exclusively on direct physical surface contact; when driven above 400°C or subjected to minor barrel imperfections, mica insulation degrades, air gaps cause localized hot spots, and uninsulated outer sheaths radiate massive amounts of wasted heat into the factory floor.
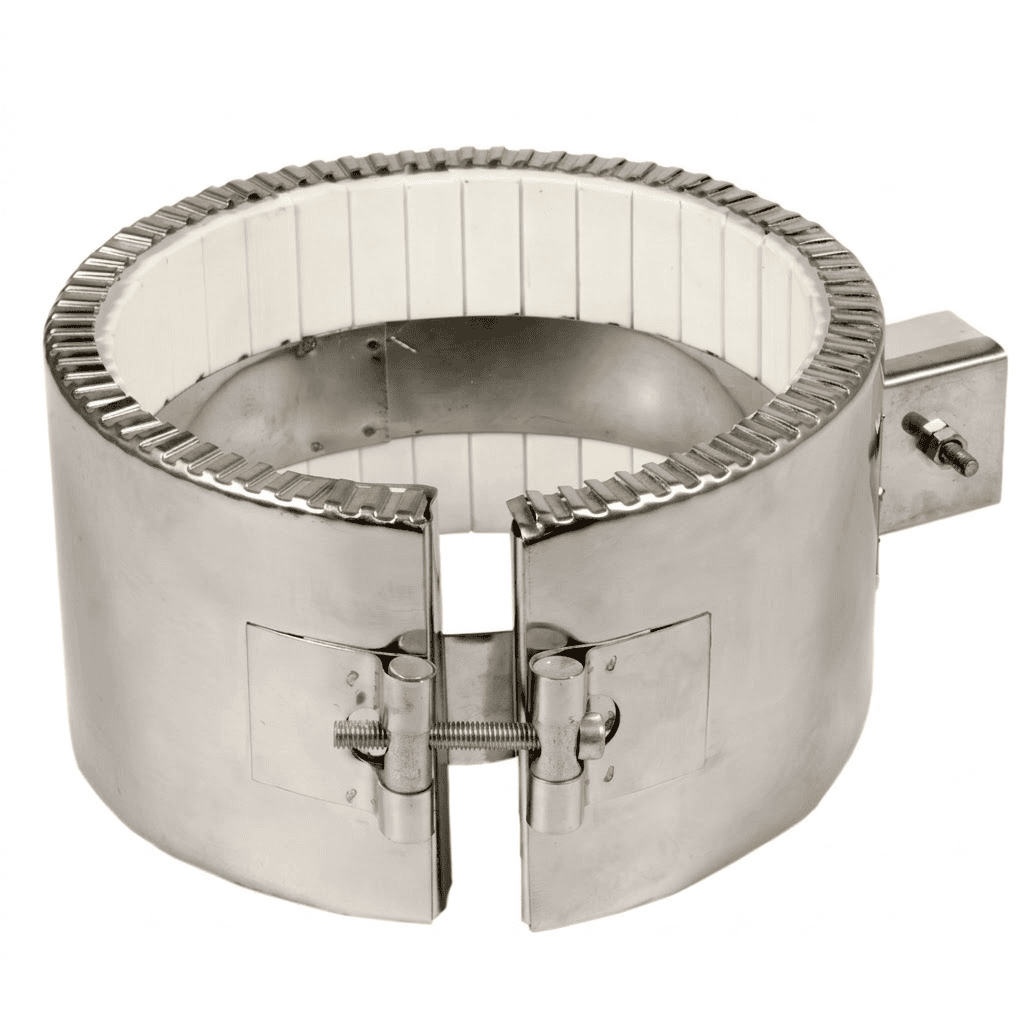
The High Temp Ceramic Band Heater For Plastic Extruder 380V overcomes both thermal ceiling and energy-loss limitations through dual-mode conductive and radiant architecture:
-
High-Temperature Interlocking Steatite Core: Heavy-duty Ni80Cr20 helical resistance coils are threaded through precision-molded, interlocking steatite ceramic knuckles. Because the wire sits inside open ceramic channels rather than being pressed tightly against a thin mica sheet, the heater transfers thermal energy via both direct conduction through the ceramic blocks and internal infrared radiation directly into the steel extruder barrel—eliminating burnout caused by minor barrel surface irregularities.
-
Integrated Ceramic Fiber Thermal Insulation: A 6mm to 12mm layer of low-thermal-conductivity ceramic fiber blanket is sandwiched between the ceramic core and the outer SUS304 stainless steel housing. This thermal barrier reduces exterior shell temperatures by up to 40%, cutting electrical power consumption by 20%–30% while protecting operators and overhead wiring from extreme radiant heat.
-
Flexible Serrated Shroud & High-Torque Clamping: Precision-serrated edges along the stainless steel outer shell allow the heater band to flex open effortlessly around large extruder barrels during installation, then pull tightly closed via heavy-duty clamping straps and socket-head barrel nuts.
- ✓ Extreme Operating Temperatures up to 750°C: Interlocking steatite ceramic blocks and heavy-gauge Ni80Cr20 helical coils handle high-melt engineering plastics where standard mica bands fail.
- ✓ 20%–30% Energy Savings via Ceramic Fiber Insulation: Built-in ceramic fiber thermal blanket drastically curtails rear heat loss, lowering kWh consumption and keeping factory ambient temperatures cooler.
- ✓ Dual Conductive & Radiant Heat Transfer: Tolerates minor barrel surface imperfections without developing hot spots, ensuring uniform melt viscosity and longer element service life.
- ✓ Serrated-Edge Flexible Stainless Shroud: Engineered with notched edges for easy wrap-around installation and high-tension clamping via heavy-duty barrel nuts.
- ✓ 380V Three-Phase & Single-Phase Industrial Wiring: Built for high-power extruder zones with protected ceramic terminal blocks, 2-pin industrial plugs, threaded studs, or armored leads.
- ✓ Direct OEM Manufacturing: Custom inner diameters (50mm to 1200mm+), widths, 380V/400V/480V power ratings, air/water cooling shrouds, and thermocouple cutouts engineered by HT HEATER.
Technical Specifications & Performance Data
| Parameter | Standard Specification | Customizable Options | Engineering Notes |
| Product Category | High Temp Ceramic Band Heater | Air-cooled / water-cooled ceramic barrel bands | Insulated conductive & radiant barrel heater |
| Operating Voltage | 380V AC (Single-Phase or 3-Phase) | 220V, 230V, 240V, 400V, 415V, 440V, 480V | Balanced delta/star 3-phase wiring for large zones |
| Power Output (Wattage) | 500W to 20kW+ per band | Mapped precisely to extruder barrel zone demand | Supports watt densities up to 6.5–8.0 W/cm^2 |
| Max Operating Temp | Up to 750°C (1382°F) | Standard continuous duty: 400°C – 650°C | Controlled via closed-loop PID / SCR power rack |
| Inner Diameter (ID) | Φ60mm to Φ800mm Standard | Large twin-screw & compounding barrels up to Φ1200mm+ | Available in one-piece, two-piece, or hinged shells |
| Band Width | 40mm to 400mm Standard | Narrow nozzle widths or multi-circuit wide zones | Modular ceramic knuckle pitch allows tailored widths |
| Outer Housing Material | Serrated SUS304 Stainless Steel | SUS316L, Aluminized Steel | Notched perimeter edges prevent buckling when flexed |
| Thermal Insulation Layer | 6mm – 12mm Ceramic Fiber Blanket | Extra-thick 15mm–25mm energy-saving jacket | Reduces outer shell temperature & cuts power loss |
| Heating Core & Ceramic | Ni80Cr20 Helical Coil + Steatite Blocks | High-temp FeCrAl resistance wire | Interlocking ceramic knuckles permit radial flexing |
| Clamping & Terminations | Heavy-Duty Barrel Nuts + Ceramic Terminal Block | 2-pin shrouded plugs, threaded studs, armored leads | Custom holes & slots for thermocouples & melt bolts |
Industrial Applications & Solutions
This insulated, 380V high-temperature ceramic band heater is the industry standard across high-output plastics and thermal processing lines:
-
Single & Twin-Screw Plastic Extruders: Powers high-temperature metering, mixing, and die-head zones for pipe, sheet, profile, film, and pelletizing extrusion lines.
-
High-Temperature Injection Molding Barrels: Melts engineering thermoplastics (PEEK, PC, PSU, Nylon, ABS) cleanly with rapid recovery and reduced electrical draw.
-
Blow Molding & Parison Extrusion Heads: Delivers uniform 360-degree circumferential heat around heavy-walled accumulator heads and die rings.
-
Chemical Reactors, Autoclaves & Pipe Heating: Provides energy-efficient external heating for high-temperature cylindrical vessels and process transfer lines.
-
Hot-Melt & Rubber Extrusion Machinery: Maintains tight viscosity control along continuous compounding and vulcanizing barrels.
HT Heater Advantage: Why Choose Our Ceramic Band Heater?
| Engineering Feature | HT Heater Ceramic Band Heater | Standard Uninsulated Mica Bands | Operational Advantage |
| Thermal Efficiency | Integrated 6mm–12mm ceramic fiber insulation jacket | Bare metal outer shell radiating heat to air | Cuts electrical energy consumption by 20%–30% and lowers external touch temperatures for improved workplace safety. |
| Temperature Ceiling | Interlocking steatite ceramic blocks rated to 750°C | Mica sheets limited to 350°C–450°C | Handles high-temperature engineering resins without dielectric breakdown or premature insulation carbonization. |
| Tolerance to Barrel Wear | Dual conductive + infrared radiant heat transfer | Requires 100% flush metal-to-metal contact | Continues operating reliably without hot-spot burnout even on older, slightly scored, or out-of-round extruder barrels. |
| Clamping & Terminal Build | Full-width SUS304 straps, barrel nuts & shrouded blocks | Thin bent tabs and exposed post terminals | Withstands repeated thermal cycling and high clamping torque on heavy industrial 380V extrusion lines. |
Installation & Handling Guidelines
-
Gentle Opening During Barrel Installation: When installing a one-piece ceramic band heater over an extruder barrel, flex the band open only wide enough to slide over the cylinder. Over-bending the band backward can crack the interlocking steatite ceramic knuckles. For large diameters (≥ Φ250 mm), specify a two-piece half-shell design.
-
Clean Barrel & Perform Hot Re-Torquing: Scrape away all burned polymer residue and scale from the barrel before mounting. Tighten the socket-head barrel nuts evenly when cold, heat the barrel to approximately 50%–75% of operating temperature, shut off 380V power, and re-torque the clamping screws to secure the band tightly against thermal expansion.
-
Keep Terminals Clear of Polymer Drool: Orient the ceramic terminal block, 2-pin plug, or armored lead exit away from the feed throat and die face so purged molten plastic cannot drip onto live electrical connections.
-
Verify 380V Phase Wiring: Confirm whether the heater is wired for 380V single-phase (phase-to-phase) or 380V three-phase (star/delta) before energizing, and ensure the stainless steel outer shroud is properly grounded to the extruder frame.
Customer Success Stories
Case 1:
Twin-Screw Compounding & Pelletizing Extruder OEM (Germany)
-
Application: 380V three-phase barrel zones operating continuously at 420°C–460°C for glass-filled PEEK and PPS engineering polymer compounding.
-
Challenge: Standard mica band heaters failed within 6 to 8 weeks due to extreme barrel temperatures, while radiant heat from uninsulated barrels overloaded the plant’s HVAC cooling system.
-
Solution: Partnered with HT HEATER to equip all barrel zones with 380V High Temp Ceramic Band Heaters featuring 10mm ceramic fiber insulation blankets, serrated SUS304 shrouds, and shrouded ceramic terminal blocks.
-
Results: 26% REDUCTION IN EXTRUDER POWER DRAW & 24+ MONTH LIFESPAN. External heater surface temperatures dropped by over 110°C, slashing factory cooling loads while maintaining barrel zone stability within ±1.0°C.
Case 2:
HDPE Pipe & Profile Extrusion Manufacturer (United States)
-
Application: 380V barrel and die-head heating across six large-diameter (Φ200mm–Φ350mm) single-screw pipe extrusion lines running 24/7.
-
Challenge: Minor barrel surface wear on older extruders caused air gaps under rigid mica bands, resulting in frequent hot-spot burnouts and costly unscheduled line restarts.
-
Solution: HT Heater supplied custom two-piece 380V high-temp ceramic band heaters with factory-punched thermocouple cutouts and heavy-duty barrel-nut clamping straps.
-
Results: UNSCHEDULED HEATER BURNOUTS ELIMINATED. The dual conductive and radiant heat transfer of the ceramic core bridged minor barrel imperfections effortlessly, cutting annual energy and maintenance costs across all six lines.
Pricing & Procurement Options
- OEM Customization: Tailored shapes, custom cutout holes for pipe nozzles, specialized voltage/wattage configurations, and custom strap lengths.
- Lead Times: Custom samples: 3–5 working days. Bulk production orders: 8–12 working days upon technical drawing sign-off.
- Packaging & Shipping: Individually bagged with protective foam padding and packed into heavy-duty 5-ply export cartons to prevent bending or lead wire stress during international transit.
- Minimum Order Quantity (MOQ): Low MOQ starting at 5–10 units for custom dimensions; competitive volume pricing tiers for equipment manufacturers.
Global Certifications & Compliance
- CE Marking
Fully compliant with European safety and environmental standards. - LVD Compliance
Low Voltage Directive tested for continuous thermal load safety. - RoHS Compliant
Constructed using environmentally safe, lead-controlled brass alloys. - ISO 9001
Certified quality control covering CNC machining, coil pressing, and electrical testing.
Quality Documentation: Certificate of Conformity (COC) and insulation resistance test reports included.
Comprehensive After-Sales Support
-
- Warranty: 1-Year Comprehensive Warranty covering internal heating element and built-in sensor.
-
Technical Support: Application engineers available for wattage distribution calculation, thermocouple calibration, and nozzle fitting assistance.
-
Global Response Network: BACKED BY 30+ YEARS MANUFACTURING EXPERIENCE with technical inquiry feedback within 2 hours.
Ready to Optimize Your Injection Molding?
Next Steps:
- 📧 Request Custom Quote – Send your nozzle dimensions, wattage, voltage, and HT-CLW-450 drawing requirements.
- 🔧 Free Design Consultation – Work with our thermal engineers to optimize heat distribution and lead insulation.
- 📦 Order Test Samples – Evaluate thermal performance on your injection molding machine.
- 📞 Contact Hot Runner Experts – Response within 2 hours
-
Leading Manufacturer & Export of Industrial Heaters
Providing A One Stop Solutions To All Industrial Heaters Needs
SINCE 1990 Professional Heater Producer | Our Products Undergo Multiple Rigorous Quality Checks